Advisory before cutting
Every RFQ comes back with a number and notes on the tolerances that actually drive cost — not a request for more information. Where a feature is expensive for no functional reason, we say so.
Nineteen Swiss-type CNC lathes and nothing else. We machine bar from Ø3.0 to 32 mm around the clock, verify every critical feature on an in-house Hexagon CMM, and return a price — with DFM notes — within 48 hours of receiving your drawing.
We are a Swiss-only shop floor. That focus decides how we advise, how we route work, and what leaves the building with every shipment.
Every RFQ comes back with a number and notes on the tolerances that actually drive cost — not a request for more information. Where a feature is expensive for no functional reason, we say so.
14 Japanese-built machines (Citizen Cincom, Tsugami) take the tight-tolerance and complex work; 5 Chinese-built machines (TODAYCNC, SOWIN) run volume. Work is allocated by tolerance class, not by which machine happens to be free.
Dimensional report, ballooned first-article inspection, EN 10204 3.1 material certificate, roughness records and RoHS / REACH declaration ship with every order — not on request.
Every machine carries a sub-spindle and driven tooling, so front and back working are completed in one cycle. The fleet covers Ø3.0–32 mm bar; 19 of 19 machines handle ≤Ø20 mm work.
| Brand | Model | Qty | Max bar Ø | Control |
|---|---|---|---|---|
| Citizen Cincom | L20E-2M10 | 6 | Ø20 mm (Ø25 option) | 6-axis |
| Citizen Cincom | L32 | 2 | Ø32 mm | 5-axis |
| Tsugami | B0205 | 6 | Ø20 mm | 5-axis |
| TODAYCNC | TC32 series | 2 | Ø32 mm | 5-axis |
| SOWIN | SZ-20 series | 3 | Ø25 mm | 5–6-axis |
| Total | 19 | Ø3.0 – 32 mm | — | |
Real machines, real coolant, real parts in the green trays. This is the shop that will run your order.
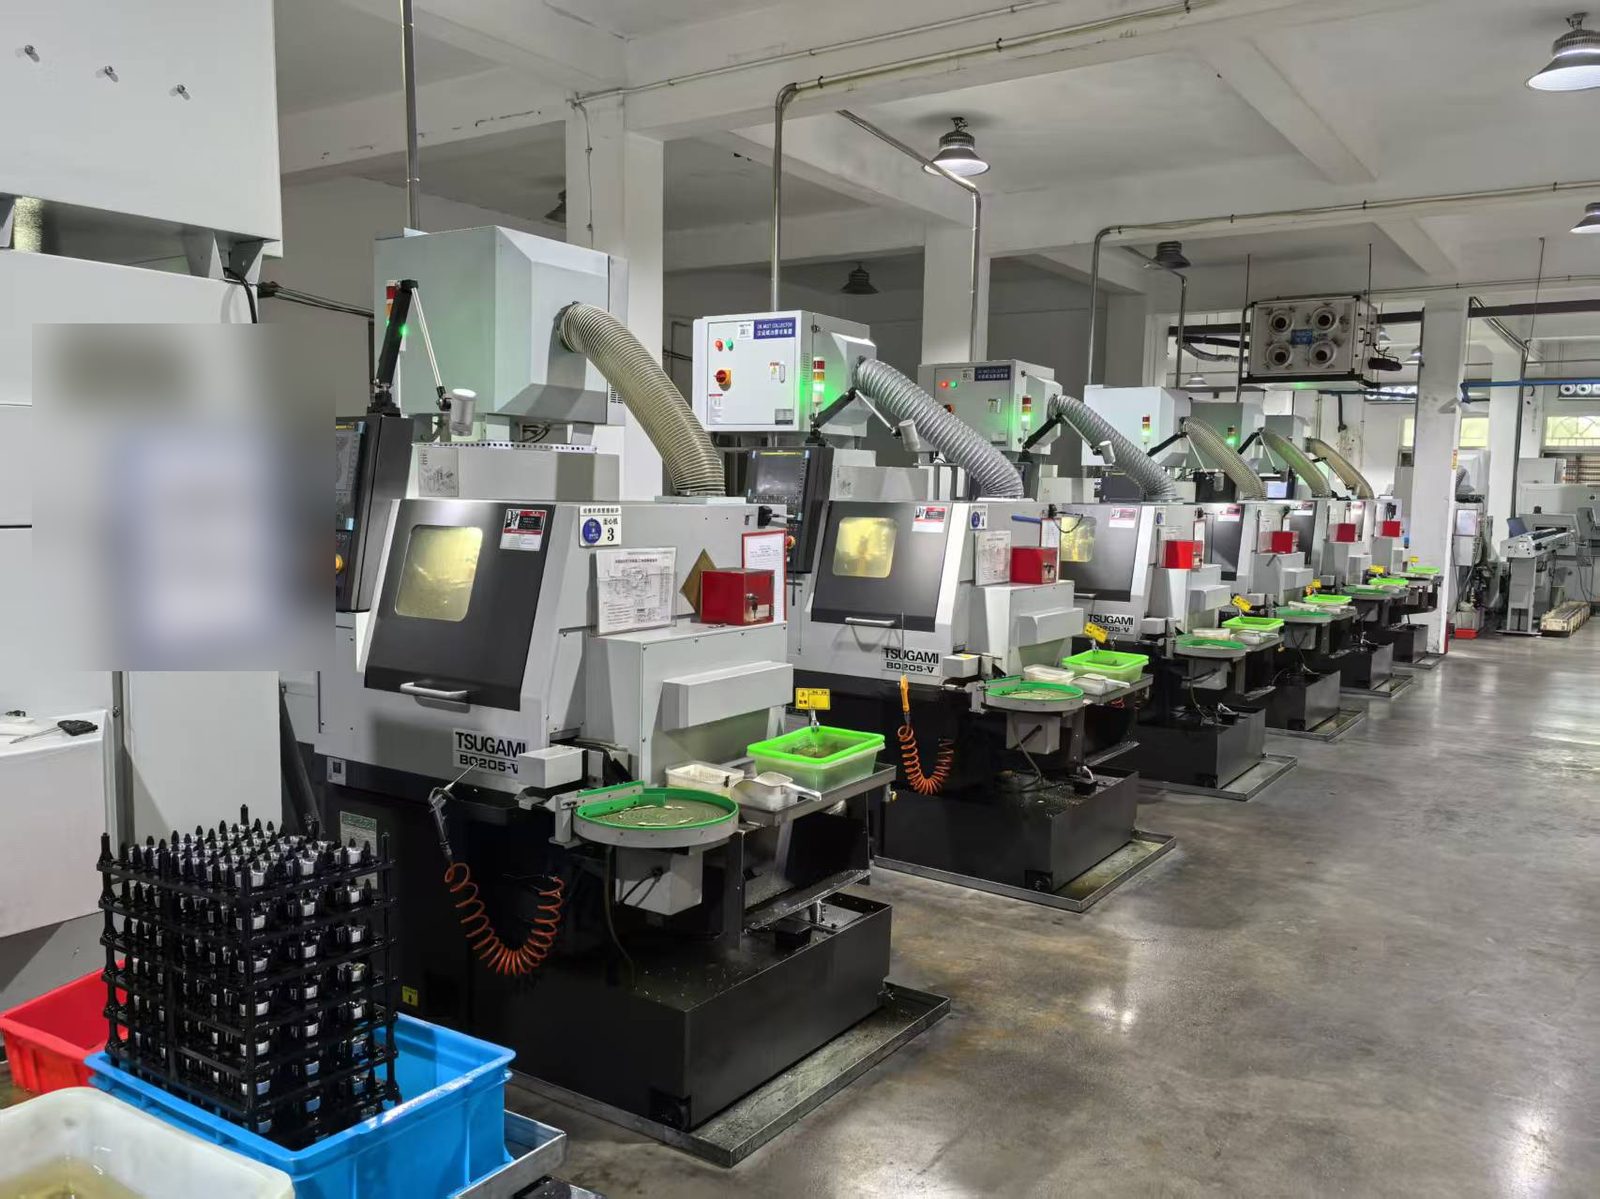
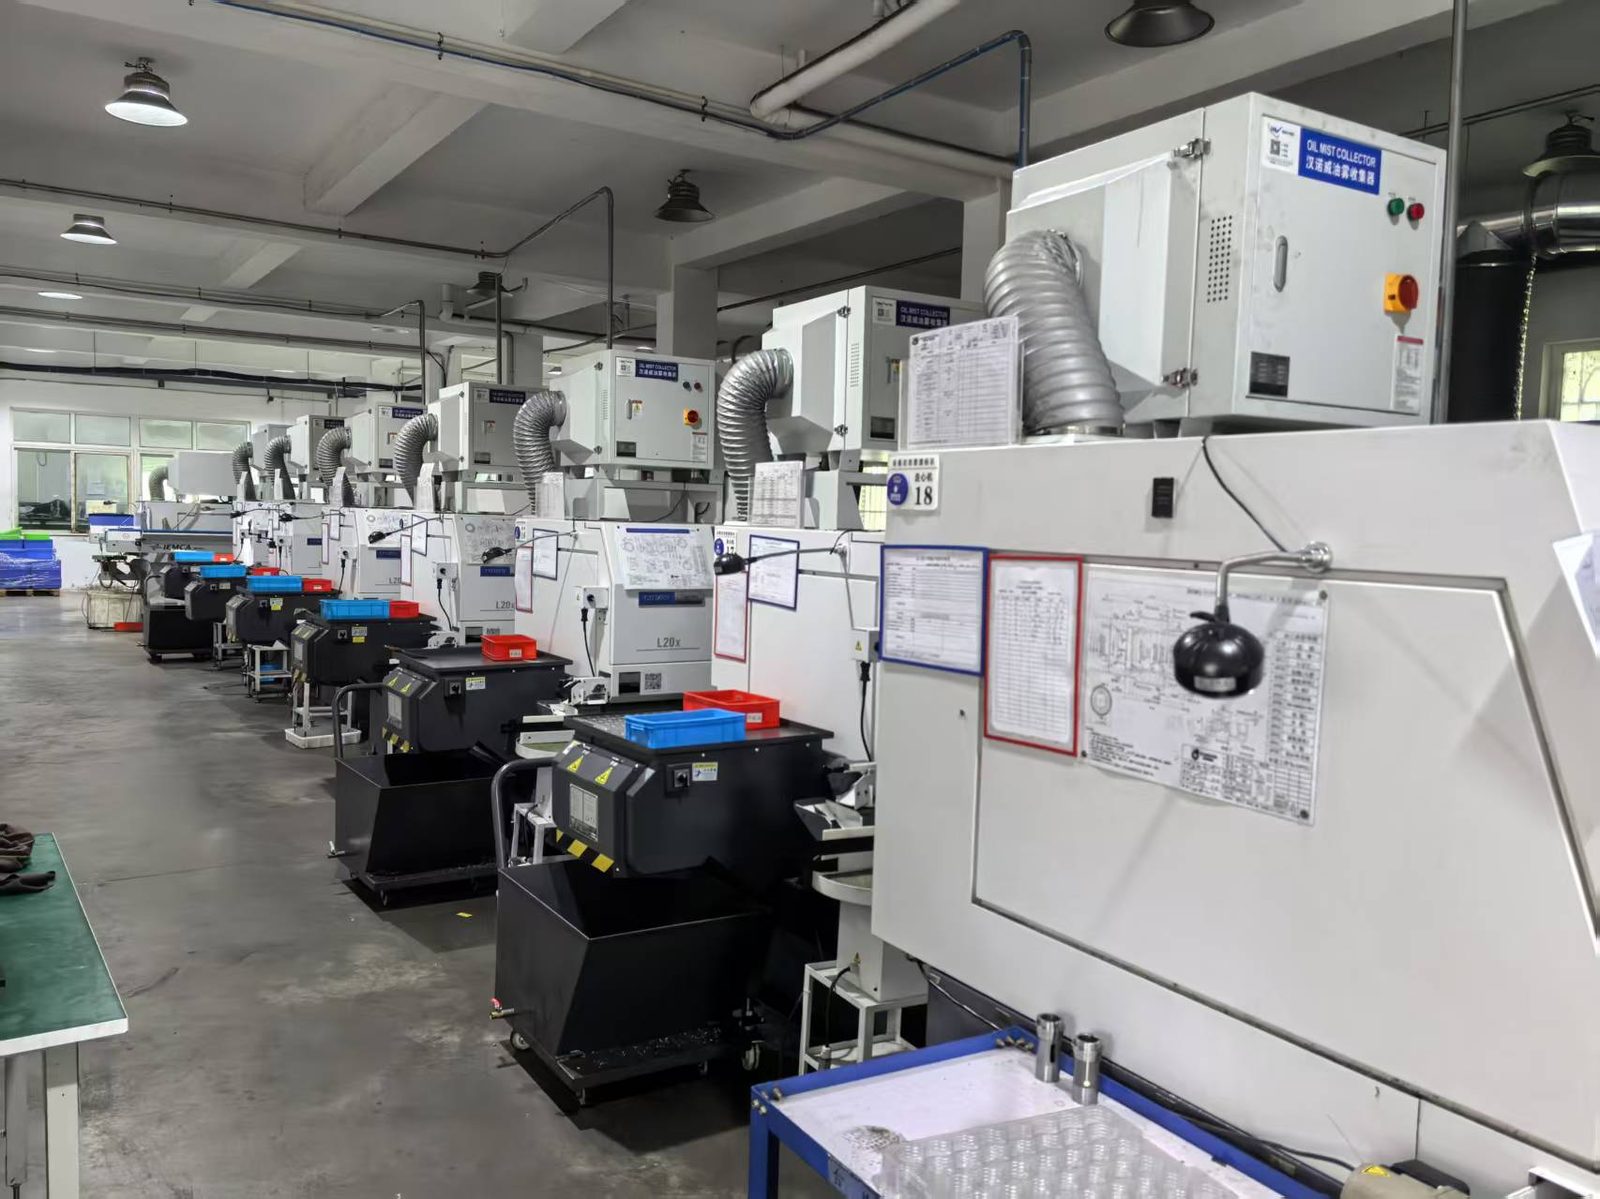
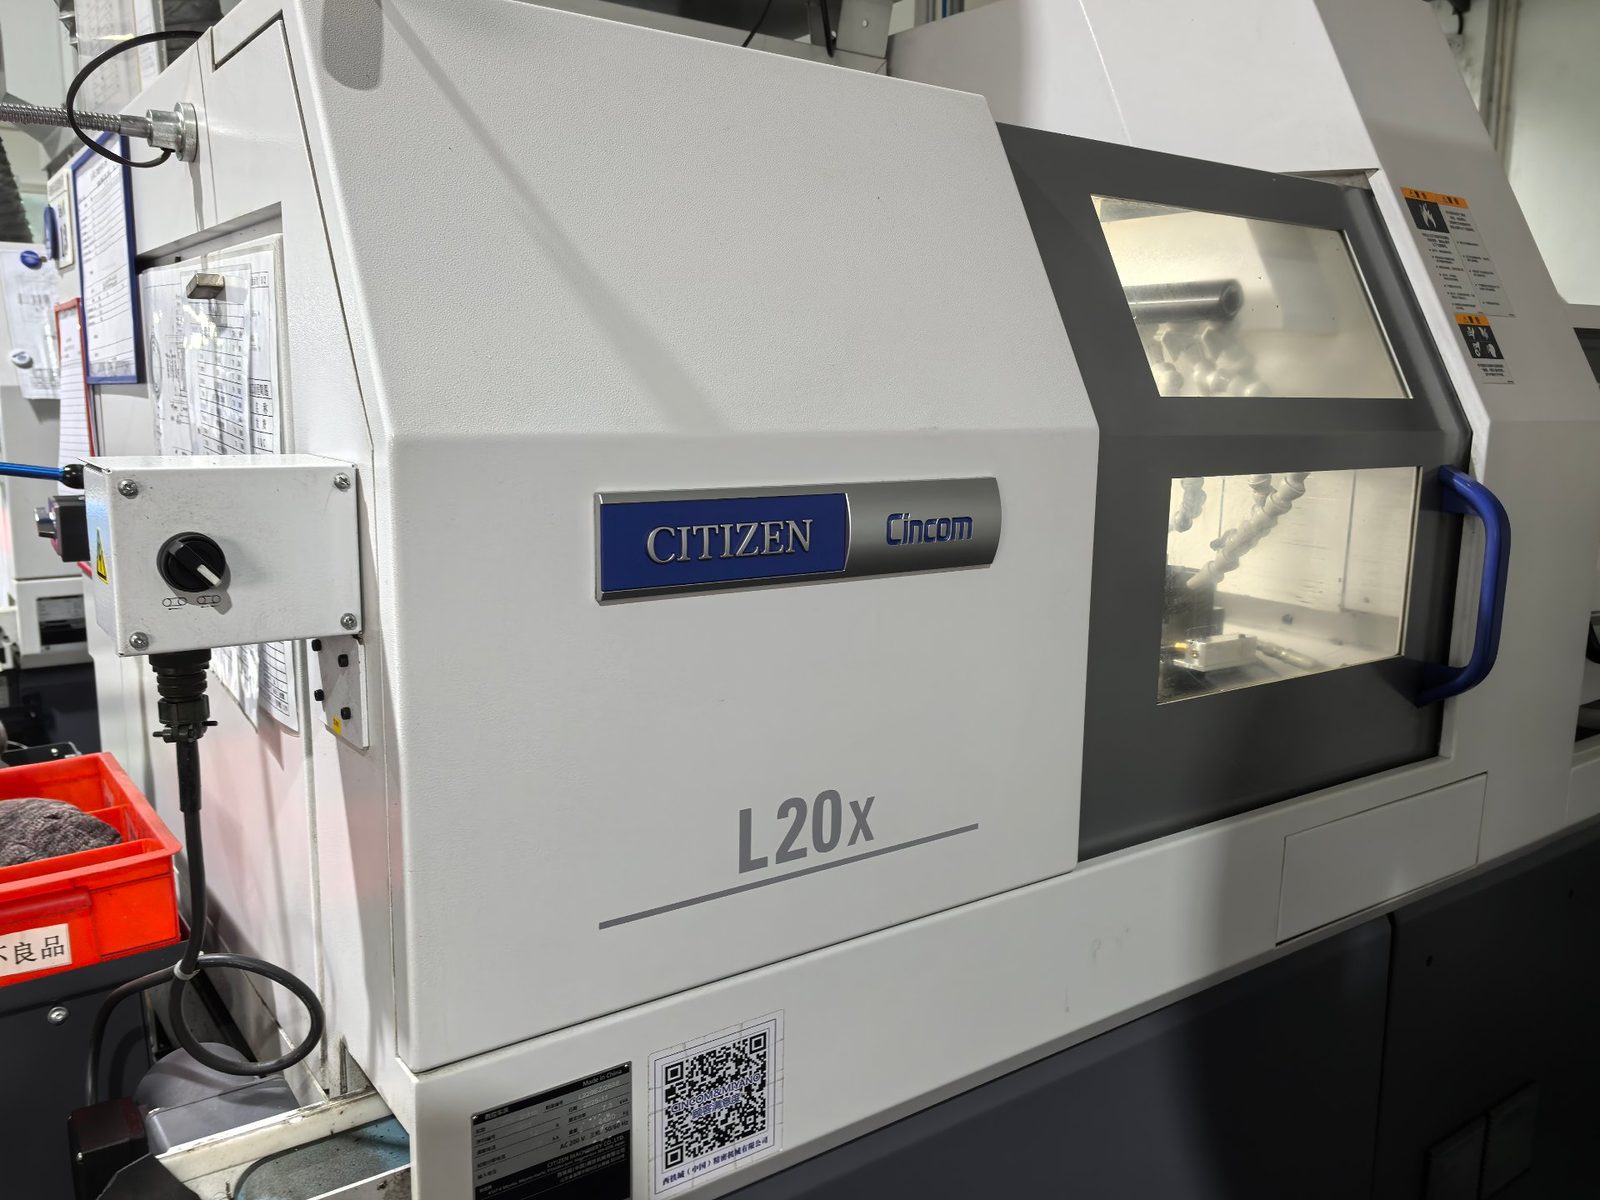
The ±0.005 mm figure is a diameter capability: turned diameters on parts ≤ Ø32 mm from ground or peeled bar (h6–h9), on a temperature-controlled floor at 20 ± 2 °C with chilled coolant, verified by in-process SPC at Cpk ≥ 1.33 and confirmed on the CMM. Positional, concentricity, thread and deep-bore features are quoted against the drawing, feature by feature.
A patrol inspector and a CMM inspector cover every shift. Patrol inspection runs on a two-hour cycle across all 19 machines with recorded results; first-piece and last-piece of every batch are verified in the metrology room. Night shift carries the same cover as day shift — no production runs without inspection.
Dimension by dimension, ballooned and indexed to your drawing numbers.
CNAS-accredited, traceable to national standards. Certificates on file with expiry dates.
Mill test certificates to EN 10204 3.1 with every shipment, bar heat number to finished lot.
Inspection records kept against the lot number and available on request.
CMM, contour / form, roughness and hand-gauge metrology are all in-house. We do not subcontract inspection, so the report matches the part.
19 sliding-headstock lathes and nothing else. Small diameter, high length-to-diameter, multi-operation parts are our only business.
Every RFQ gets a number plus notes on tolerances that drive cost — not a request for more information.
Currently in production: precision turned components for AI data-centre liquid-cooling assemblies, and automotive turned components.
| Family | Grades in regular use |
|---|---|
| Stainless steel | 303 / 304 / 316 |
| Aluminium | 6xxx series · 2xxx series |
| Free-cutting steel | 12L14 / 1215 |
| Brass & copper | Brass · Tin bronze · Pure copper |
A STEP file plus a dimensioned PDF with GD&T is enough to start. We return a quotation with DFM notes. Mutual NDA signed before any drawing is exchanged, on request.